

Molded Pulp Quality Control: Moisture, Dimensional Tolerance and Test Standards
Buyers often ask what separates a good molded pulp tray from a poor one. The answer is rarely visible at first glance. Quality in molded pulp is defined by a handful of measurable properties: moisture content, wall thickness consistency, dimensional tolerance, surface condition and mechanical strength. This guide explains each one, what is achievable in production, and how to verify it before committing to a supplier.
The Five Quality Indicators That Matter
1. Moisture Content
Moisture is the most overlooked quality factor in molded pulp. Parts dried too little will warp, grow mold in transit or lose stiffness; parts dried too hard become brittle and crack. Typical production ranges:
| Process | Typical Moisture Content | Why It Matters |
|---|---|---|
| Dry press | 6-9% | Balances strength and flexibility |
| Wet press | Lower, tighter range | Needed for long-term dimensional stability |
A stable moisture level also affects how trays behave during humid ocean freight. Reliable suppliers measure moisture and adjust drying settings rather than guessing.
2. Wall Thickness Consistency
Because pulp forms on a mesh surface, wall thickness is uniform only when the tool, slurry and vacuum are correctly balanced. Thin spots appear where fiber deposits weakly, usually at deep corners or under ribs. For dry press parts, 2-3 mm walls are typical; wet press can reach 1.5-2.5 mm with better consistency.
3. Dimensional Tolerance
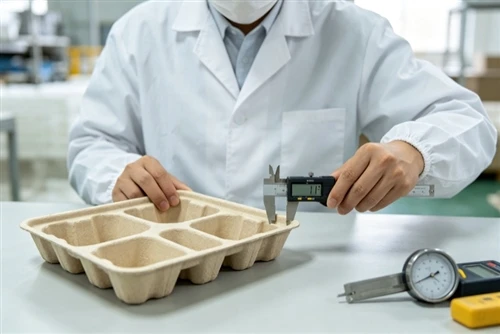
Packaging parts do not need injection-grade precision, but they need a predictable fit. Standard achievable tolerances are about ±0.5-1.0 mm on critical dimensions. Tighter tolerances are possible with wet press and careful tooling, at a higher cost.
4. Surface Condition
The surface defects that matter are: mesh marks (acceptable on functional cushioning surfaces), cracks, flash at mold parting lines, and loose fiber. For cosmetic parts, wet press gives the smooth surface buyers expect; dry press surface is textured but perfectly acceptable where the tray is hidden.
5. Mechanical Strength
Strength is verified by testing, not by feel: drop tests (for example 0.75-1.0 m onto concrete for lightweight electronics), compression tests for stacked trays, and edge crush or flexural checks for heavy parts.
Common Defects and Their Causes
| Defect | Typical Cause | How to Prevent |
|---|---|---|
| Warping | Uneven drying, surface drying too fast | Gradual drying, controlled humidity |
| Thin spots | Poor vacuum distribution, worn mesh | Tool maintenance, slurry control |
| Cracks | Over-drying, weak fiber, sharp tool geometry | Moisture control, design with radii |
| Flash / burrs | Mold parting lines, worn seals | Regular tool inspection |
| Loose surface fiber | Low refining, poor formation | Slurry quality, forming parameters |
The Factory QC Flow
A reliable supplier runs checks at four stages:
- Incoming material: pulp and recycled paper quality, brightness, contamination
- In-process: wall thickness sampling, visual inspection at the forming station, moisture spot checks during drying
- Finished goods: dimensional measurement with gauges, moisture reading, drop and compression tests on samples
- Pre-shipment: final visual inspection, packaging condition, carton weight verification
What to Ask a Supplier Before Ordering
Before placing a custom molded pulp order, request:
- A sample or first article with actual moisture and dimension data
- Their standard tolerances for the part size you need
- Drop or compression test results for a similar product
- Their inspection process, and whether third-party inspection is available
Hesheng Innovation Development Ltd. has manufactured custom molded pulp and molded fiber packaging since 2013, with in-house tooling, full process control and routine moisture, dimensional and strength testing. For a quality review of your specific part, send your drawing or a sample through the contact page.
FAQ
Q: What is the ideal moisture content for molded pulp packaging?
A: For dry-pressed molded pulp, moisture content is typically held between 6% and 9%. Wet-pressed products leave the press at a lower moisture level, which improves dimensional stability and surface finish.
Q: What wall thickness can molded pulp packaging achieve?
A: Dry-pressed parts are generally up to about 3 mm thick, while wet-pressed parts typically range from 1.5 to 2.5 mm. Wall thickness is controlled by mold design, pulp consistency and press parameters.
Q: What dimensional tolerance should I expect for custom molded pulp?
A: A practical tolerance is about ±0.5 to 1.0 mm on key dimensions, depending on part size and process. Wet pressing holds tighter tolerances than dry pressing.
Q: How does Hesheng control molded pulp quality?
A: Hesheng runs a four-stage QC process: incoming fiber inspection, in-process checks on moisture and wall thickness, dimensional and surface inspection of finished parts, and final AQL-based sampling before packing.


